Why Confectionery Producers Need Advanced Weighing Systems
Confectionery manufacturers face constant pressure to increase output while maintaining strict quality standards. Whether producing candies, gummies, chocolates, cookies, or snack products, accurate weight control directly impacts profitability and customer satisfaction.
Traditional weighing systems often struggle to keep pace with today’s high-speed production environments. As production capacities continue to grow, many manufacturers are investing in multi-channel checkweighers to improve inspection efficiency without sacrificing accuracy.
These advanced systems allow multiple product streams to be inspected simultaneously, making them ideal for modern confectionery packaging operations.
What Is a Multi-Channel Checkweigher?
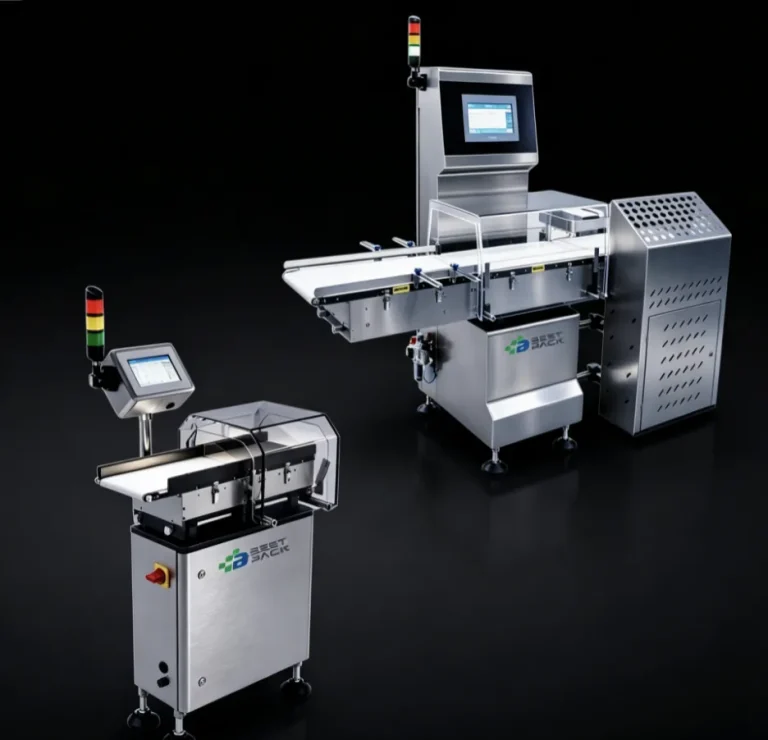
A multi-channel checkweigher is an automated weighing solution designed to inspect several product lanes at the same time.
Instead of using a single weighing lane, the machine can monitor multiple product flows simultaneously, significantly increasing inspection capacity.
Typical workflow includes:
Product Distribution
Products are automatically separated into multiple channels.
Dynamic Weighing
Each lane independently performs high-speed weight inspection.
Data Comparison
The system compares actual weights against target specifications.
Automatic Rejection
Packages outside acceptable tolerances are removed automatically.
Common Applications in Confectionery Production
Gummy Candy Packaging
Weight consistency is critical for retail compliance and consumer trust.
Chocolate Packaging
Multi-lane inspection supports high-volume production while maintaining accuracy.
Biscuit and Cookie Packaging
Manufacturers can inspect multiple product streams simultaneously.
Snack and Promotional Packs
Mixed product packages benefit from automated weight verification.
Advantages of Multi-Channel Checkweighers
Increased Inspection Capacity
Multiple lanes dramatically increase throughput compared to single-channel systems.
Improved Accuracy
Advanced weighing sensors deliver precise measurements even at high speeds.
Reduced Product Giveaway
Manufacturers avoid unnecessary overfilling and material waste.
Enhanced Quality Assurance
Every package is inspected before reaching customers.
Supporting High-Speed Packaging Lines
Modern confectionery facilities often operate multiple packaging lines around the clock.
Multi-channel checkweighers help support:
Continuous Production
Inspection keeps pace with fast-moving packaging equipment.
Automated Quality Control
Manual weight checks are minimized.
Reduced Labor Requirements
Automation decreases dependence on manual inspection processes.
Better Production Visibility
Real-time monitoring improves operational control.
Industry 4.0 Features
Leading checkweigher systems now include:
Production Data Collection
Weight information is stored automatically.
Performance Analysis
Operators can identify trends and optimize processes.
Remote Monitoring
Managers can monitor production performance from multiple locations.
Intelligent Reporting
Automated reports simplify quality audits and compliance documentation.
Why Confectionery Manufacturers Are Upgrading Their Inspection Systems
Growing product diversity and higher consumer expectations require better quality control technologies.
Modern manufacturers seek equipment that offers:
- Higher throughput
- Better accuracy
- Greater automation
- Lower operating costs
- Improved traceability
Multi-channel checkweighers address all of these requirements while supporting future production growth.
Choosing the Right Multi-Channel Checkweigher Manufacturer
Important considerations include:
Weighing Accuracy
The system must meet product-specific tolerance requirements.
Production Capacity
Equipment should accommodate both current and future production volumes.
Integration Capability
The machine should connect seamlessly with existing packaging lines.
Technical Service
Reliable support minimizes downtime and maximizes productivity.
Conclusion
Multi-channel checkweighers provide confectionery manufacturers with an efficient solution for high-speed weight inspection. By improving accuracy, reducing product giveaway, and supporting automated quality control, these systems help producers achieve higher operational efficiency and stronger product consistency.