Why Beverage Producers Are Investing in Automated Case Packing
As global demand for bottled water, carbonated drinks, juices, dairy beverages, and energy drinks continues to grow, manufacturers are under increasing pressure to improve productivity while maintaining packaging quality.
While filling and labeling operations are already highly automated in most beverage plants, end-of-line packaging often remains a bottleneck. Manual case packing can create labor challenges, inconsistent packaging quality, and production slowdowns.
To overcome these issues, many manufacturers are adopting side loading case packers as part of their automated end-of-line packaging systems.
These machines provide efficient, reliable, and scalable solutions for loading products into shipping cases and cartons.
What Is a Side Loading Case Packer?
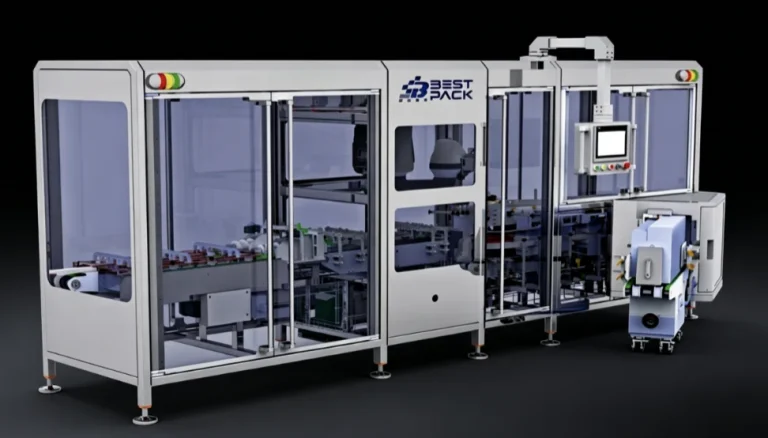
A side loading case packer is an automated packaging machine that groups products and inserts them horizontally into pre-formed cartons or cases.
Unlike top loading systems, products enter the case from the side, making the machine particularly suitable for rigid containers and high-speed packaging applications.
The process generally includes:
Product Collation
Products are grouped into predefined configurations.
Case Preparation
Corrugated cases are erected and positioned automatically.
Side Loading Operation
Products are transferred horizontally into the case.
Case Closing
The filled case is sealed and discharged for palletizing.
This automated process significantly improves efficiency and consistency.
Applications in Beverage Packaging
Bottled Water Packaging
Side loading case packers efficiently handle:
- Single-serve bottles
- Multi-bottle packs
- Retail-ready shipping cases
Carbonated Soft Drinks
The machines support high-speed production lines where reliability and throughput are essential.
Juice Packaging
PET bottles, glass bottles, and cartons can all be packed automatically.
Dairy Beverage Products
Milk drinks, yogurt beverages, and protein shakes require secure transportation packaging, making automated case packing an ideal solution.
Advantages of Side Loading Case Packers
High-Speed Production
Modern case packers can keep pace with today’s fast beverage filling lines.
Reduced Labor Requirements
Automation minimizes manual handling and lowers labor costs.
Consistent Case Quality
Every case is loaded according to predefined specifications.
Improved Workplace Safety
Reducing manual lifting and repetitive tasks improves operator safety.
Why Side Loading Designs Are Popular in Beverage Industries
Efficient Product Handling
Bottles and containers remain stable during loading.
Flexible Pack Patterns
Manufacturers can create a wide variety of case configurations.
Compact Footprint
Many side loading systems require less floor space than alternative solutions.
Reliable Continuous Operation
The design supports high-volume manufacturing environments.
Integration with Complete End-of-Line Packaging Systems
A side loading case packer often operates as part of a fully automated packaging line.
Upstream Equipment
The machine can connect with:
- Shrink wrapping machines
- Cartoning systems
- Checkweighers
- Product accumulation conveyors
Downstream Equipment
After case packing, products can move directly to:
- Case sealers
- Palletizers
- Stretch wrappers
- Warehouse automation systems
This creates a seamless packaging workflow from production to shipment.
Supporting Sustainable Packaging Initiatives
Sustainability is becoming increasingly important in beverage manufacturing.
Modern case packing solutions support environmental goals through:
Optimized Carton Usage
Precise case packing minimizes wasted packaging materials.
Improved Logistics Efficiency
Well-packed cases improve pallet utilization and transportation efficiency.
Reduced Product Damage
Better packaging stability reduces waste caused by damaged products.
Compatibility with Recyclable Packaging
Machines can accommodate environmentally friendly corrugated materials.
Industry 4.0 and Smart Case Packing Technology
Advanced side loading case packers now incorporate intelligent automation features.
Real-Time Production Monitoring
Operators can track machine performance and production output.
Predictive Maintenance
Sensors help identify maintenance needs before breakdowns occur.
Automated Production Reporting
Manufacturers gain valuable insights into packaging efficiency.
Integration with Factory Management Systems
Production data can be shared across the entire facility.
Choosing the Right Case Packer Manufacturer
Several factors should be considered when selecting a supplier.
Production Capacity
The equipment should support both current and future output requirements.
Product Compatibility
Different beverage containers require different handling solutions.
Customization Capabilities
Packaging configurations vary widely across beverage categories.
Technical Support
Reliable after-sales service ensures long-term operational success.
Future Trends in Beverage End-of-Line Packaging
The beverage industry continues to evolve rapidly.
Key trends include:
Increased Automation
Manufacturers are reducing manual intervention throughout the packaging process.
Greater Packaging Flexibility
Equipment must support a wider range of product formats and promotional packaging.
Sustainable Packaging Materials
Corrugated packaging solutions continue to evolve toward improved recyclability.
Smart Manufacturing Integration
Connected packaging systems provide greater operational visibility and control.
Conclusion
Side loading case packers have become a critical component of modern beverage packaging operations. By improving efficiency, reducing labor costs, and supporting fully automated end-of-line packaging systems, these machines help manufacturers increase productivity while maintaining high packaging quality.
For beverage companies seeking scalable and reliable automation solutions, investing in a professional side loading case packer can deliver significant long-term benefits in both operational performance and packaging consistency.